Why Liquid-Cooling Pilots Stall: Seven Integration Costs to Budget Before Scale-Out

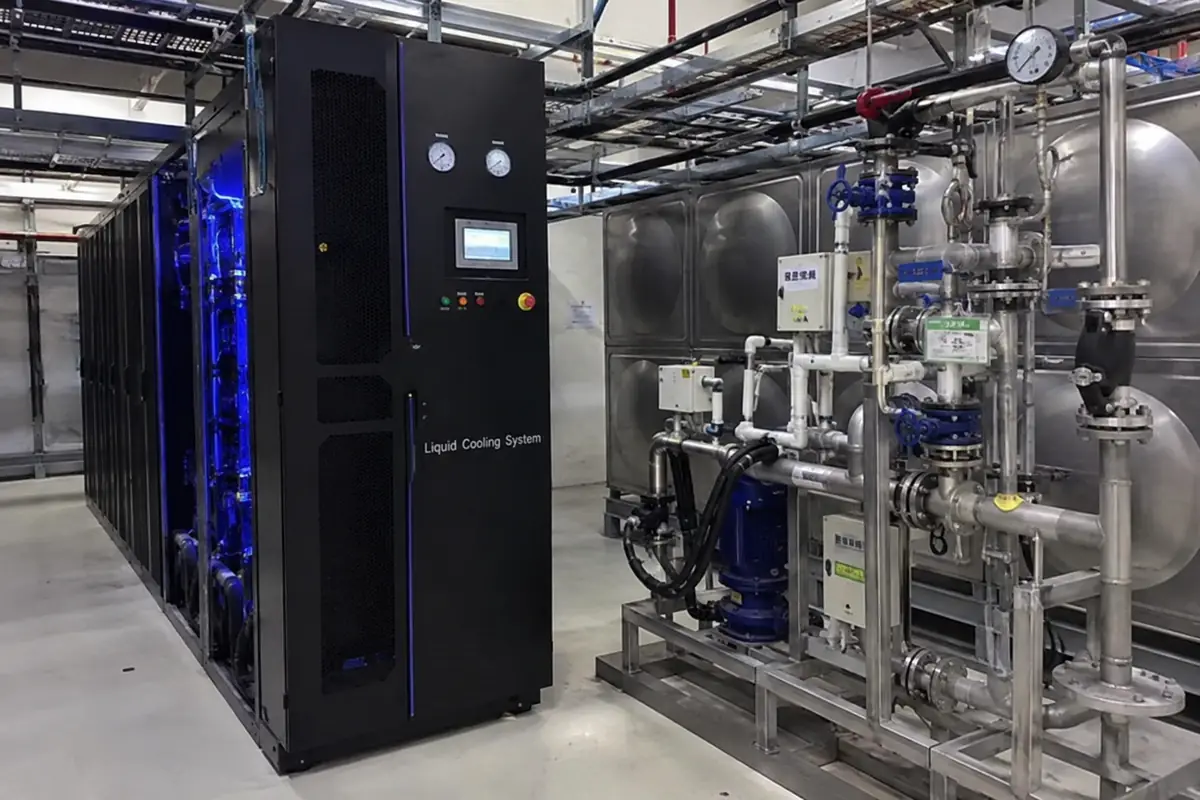
Liquid-cooling pilots often succeed technically and then slow down before production scale. The initial rack cools properly, the CDU meets its test conditions, and the facility team learns the basic controls. Yet the project still encounters delays, redesign, or unexpected operating cost when the next rows are added.
The usual cause is not that liquid cooling cannot remove the heat. It is that the pilot was funded as a hardware purchase while production requires an integrated infrastructure program.
1. The cooling boundary was drawn too narrowly
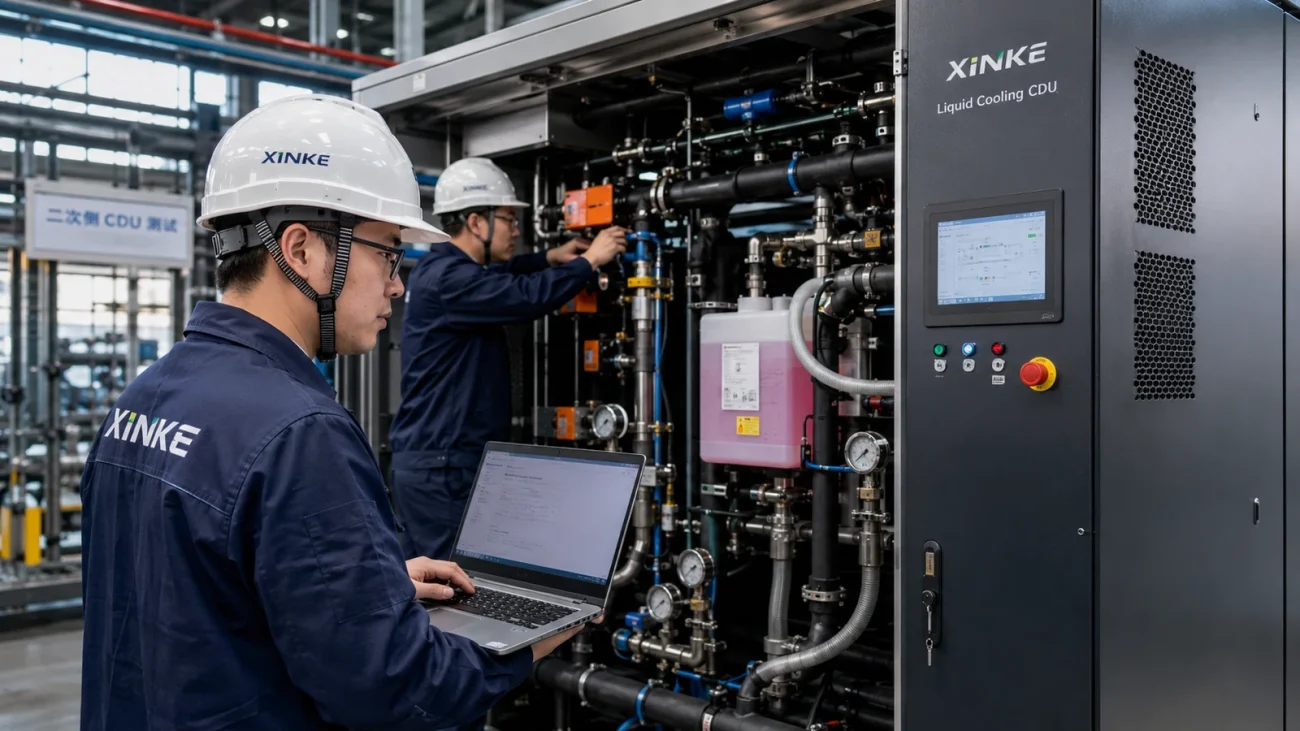
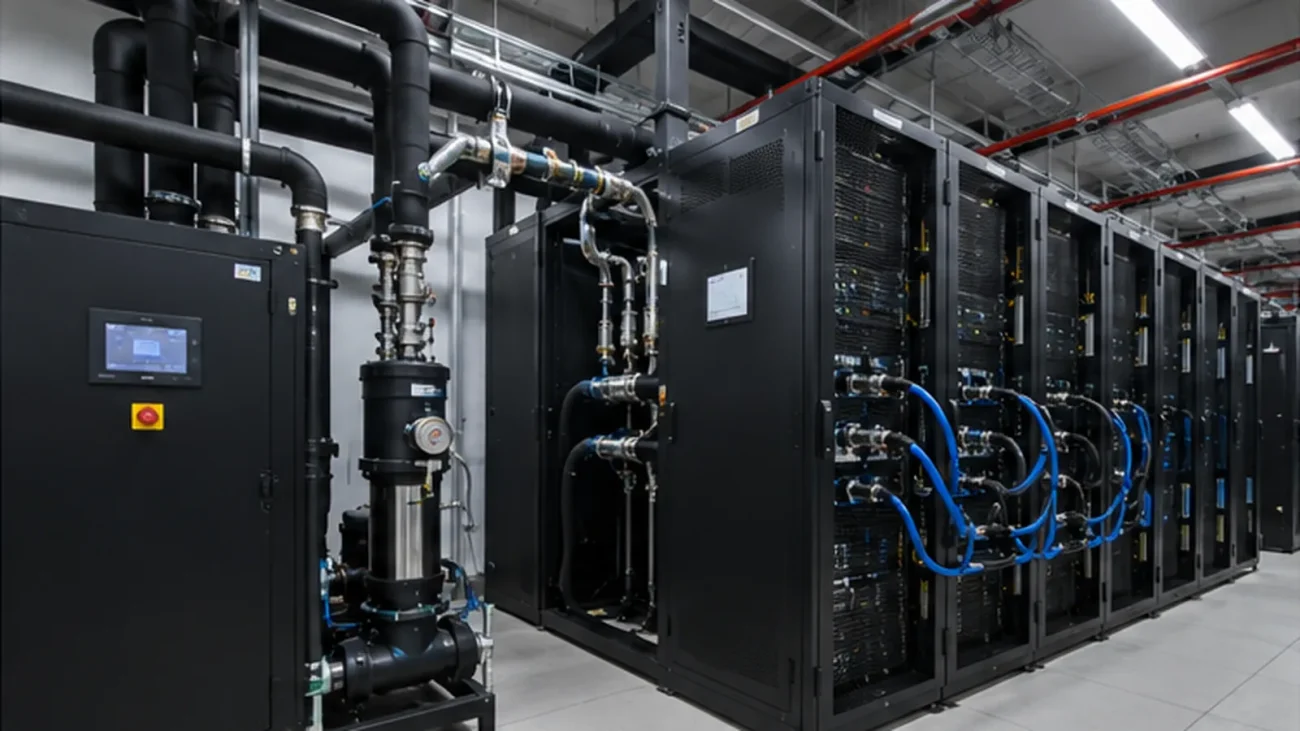
A quotation for a CDU may cover the CDU and perhaps a local piping package. A production deployment also needs rack manifolds, quick disconnects, secondary piping, facility-water connections, valves, filtration, leak detection, controls integration, power coordination, and space for service.
If the budget stops at the CDU, the first expansion reveals a gap between “equipment cost” and “installed system cost.” Build an interface matrix at the concept stage and assign a responsible party and cost center to every boundary.
- server-to-cold-plate interface;
- server or rack to quick disconnect;
- rack to manifold;
- manifold to secondary piping;
- CDU to facility-water system;
- CDU controls to BMS;
- facility heat rejection to outdoor conditions.
2. The electrical and network design was not raised with the rack density
Liquid cooling does not solve the rest of a high-density rack. The electrical distribution, protection, monitoring, cable routing, busway, transformer capacity, UPS runtime, and emergency procedures may also need changes.
High-density AI racks can also concentrate network equipment and heat in ways that are not captured by a simple “kilowatts per rack” comparison. The cooling design should coordinate with power distribution and networking so that the rack remains serviceable and has enough capacity for the intended workload.
A phased liquid-cooling plan should therefore include a rack-level services review: electrical capacity, breaker coordination, PDU layout, cable access, network switch placement, maintenance clearance, and controls cabling.
3. Facility water was treated as an unlimited boundary condition
A pilot CDU may be connected to an available chilled-water or process-water source without verifying how that source will perform when the full load is online. Production may reveal that the supply temperature rises in summer, the pressure fluctuates with other users, or the available flow is insufficient at the required CDU condition.
Define the facility-water operating envelope at each season, including:
- supply and return temperatures;
- available pressure and flow;
- water quality and filtration;
- maximum pressure at the CDU;
- redundancy and isolation arrangement;
- outdoor heat-rejection design conditions.
The CDU and heat-rejection system should be evaluated as one thermal path. A correctly sized CDU cannot maintain the required server supply temperature if the facility loop cannot reject the heat.
4. Controls integration is more than a protocol
“BMS ready” or “supports Modbus” does not tell a project whether the required points exist, how alarms are prioritized, or how the controller behaves after a communication loss. Scale-out expands the number of CDUs, valves, sensors, and alarm zones that must be coordinated.
Prepare a controls integration schedule that defines:
- protocol and physical interface;
- point names, data types, units, and update rates;
- read and write permissions;
- alarm priority and operator message;
- fail-safe behavior after a network or power interruption;
- trend retention and event-log requirements;
- cyber and access-control responsibilities.
Test the integration with the actual building system, not only with a local test client. A dashboard that displays values but cannot route a high-priority leak or pressure alarm is not operationally complete.
5. Service access and spare-parts planning arrive late
A pilot rack can be serviced using temporary access and borrowed tools. In a live data hall, every isolation point, hose, valve, filter, sensor, and quick disconnect must be accessible without compromising adjacent racks.
Add these items to both the capital plan and the operating budget:
- critical spare quick disconnects, seals, hoses, and sensors;
- filter and strainer elements;
- coolant for make-up and corrective maintenance;
- drain, transfer, and spill-handling equipment;
- training for facilities and IT teams;
- inspection tools, leak-detection testers, and calibration support.
The lowest-cost equipment package is not necessarily the lowest lifecycle cost if every routine task requires a full row shutdown.
6. The operations model is left unresolved
Liquid cooling crosses traditional organizational boundaries. The facilities team may own the CDU and heat rejection, the IT team may own the racks and workload, and a controls contractor may own the BMS. A leak alarm is not a useful warning unless all three teams agree on who investigates, who isolates, who approves a workload pause, and who authorizes restart.
Write the operating model before scale-out. It should specify:
- ownership of each system boundary;
- alarm escalation and response time;
- authorization for automatic valve closure;
- planned versus unplanned isolation procedures;
- workload notification and migration requirements;
- record retention and change control.
7. The pilot was not converted into reusable engineering standards
A successful pilot produces more than a working rack. It should produce the standards needed for the next ten racks:
- approved pipe and connector types;
- rack and manifold layout;
- supply and return temperature strategy;
- CDU and pump redundancy pattern;
- control point list and alarm matrix;
- flushing, filling, pressure-testing, and commissioning procedures;
- as-built drawing template and handover checklist.
If those outputs are not captured, every expansion becomes a new engineering project. Standardization should leave room for site-specific conditions while eliminating avoidable reinvention.
A pilot-to-production gate
Before scaling, ask whether the project can demonstrate the following:
- The complete thermal path has been tested at the design load.
- The facility-water envelope is known for the worst credible operating condition.
- The controls and BMS handle normal, degraded, and failed states.
- A rack can be isolated without taking the row offline.
- Spare parts and service procedures are available.
- Electrical and network capacity match the planned rack density.
- The operating team has practiced a leak and pump-failure response.
- Design evidence can be reused for the next phase.
If the answer to several of these questions is “we will solve that in the next phase,” the pilot has not yet become a production-ready system.
Liquid cooling scales most predictably when the project budgets for interfaces, operations, and evidence—not only cooling capacity.
XINKE LCS supports rack-mounted CDUs, sidecar CDUs, in-row CDUs, and heat-rejection equipment for phased data-center projects. For a pilot-to-production review, share the rack schedule, site conditions, facility-water constraints, controls architecture, redundancy plan, and expected expansion path.
Speak with XINKE LCS about your liquid-cooling pilot and scale-out plan.